Injection moulding cells
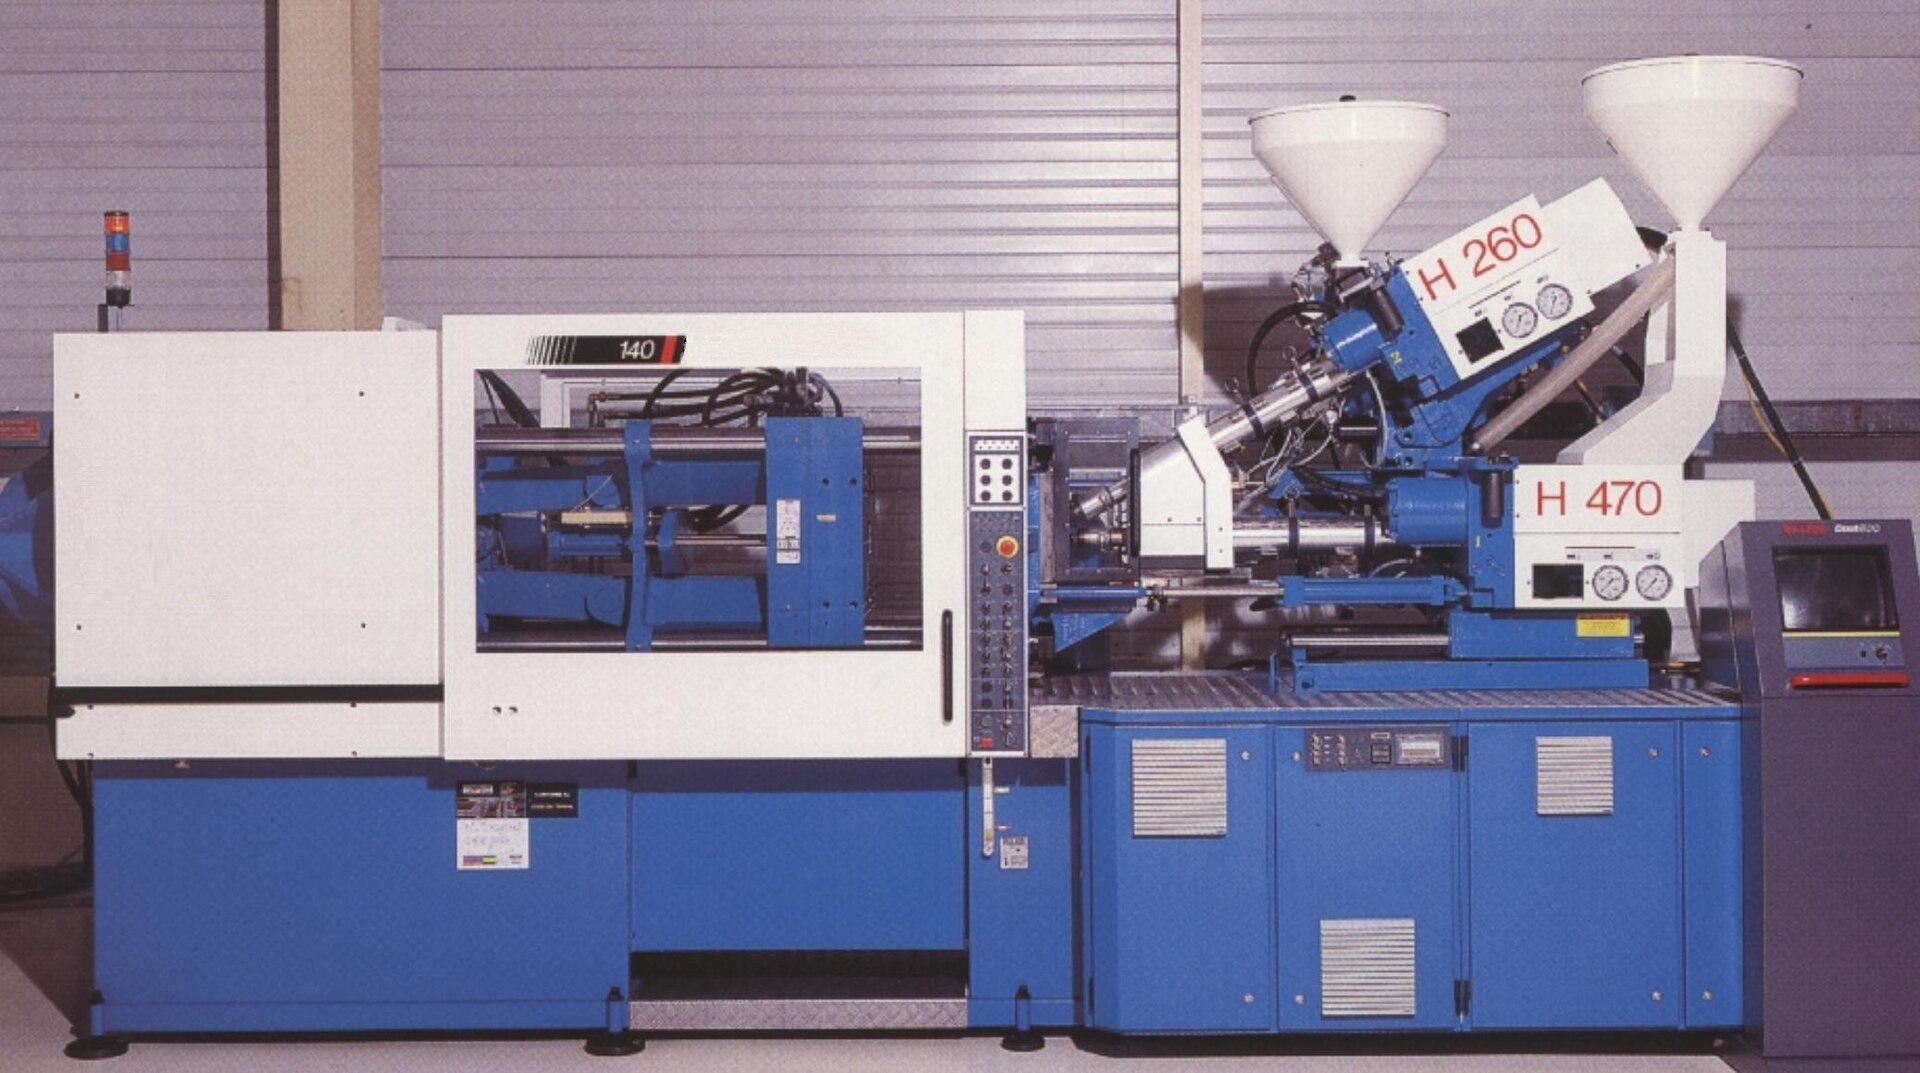
Household, industrial, electrical and packaging parts; press, mould, robot, dryer, dosing, cooling and inspection.
 CHINA BENTEINDUSTRY GROUP
Integrated plants for rigid and flexible packaging, plastic conversion, printing, filling interfaces and final packing.
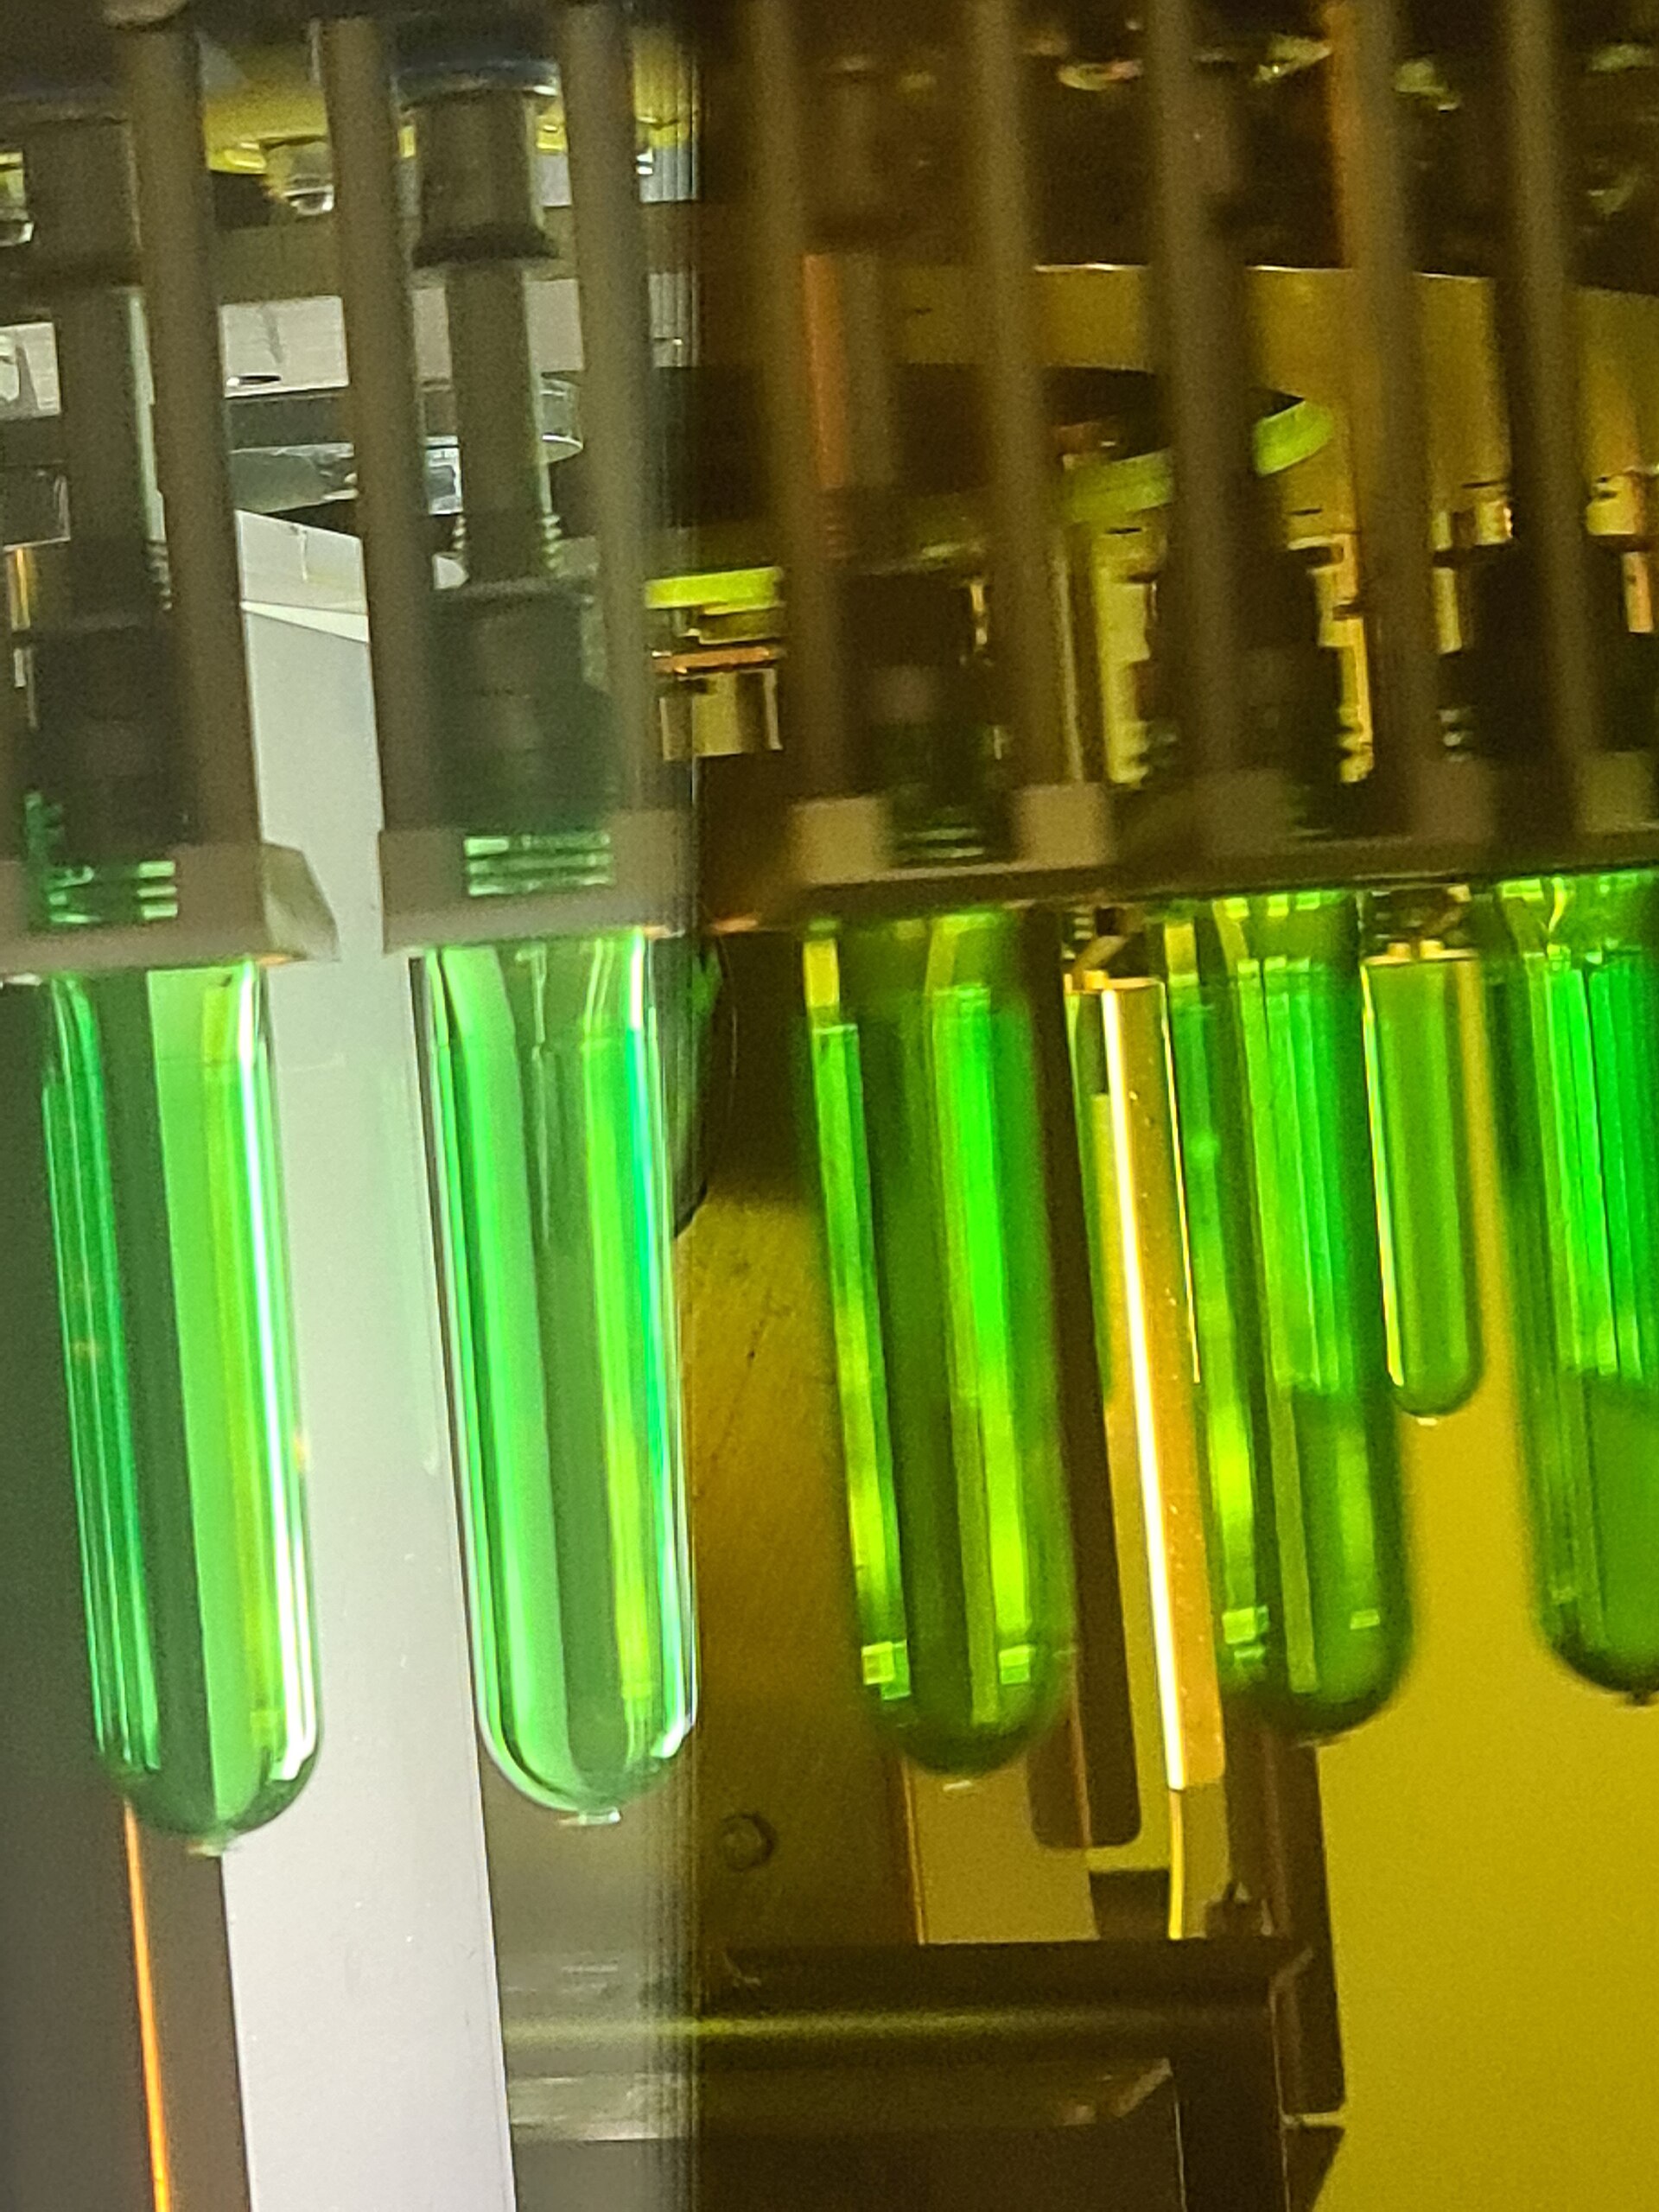
China Bente configures packaging and plastics plants around the actual product—not one generic “plastics line.” Scope can include injection moulding, pipe/profile/sheet or film extrusion, extrusion blow moulding, PET stretch blow moulding, mould and die manufacture, utilities, recycling and final packing.
Household, industrial, electrical and packaging parts; press, mould, robot, dryer, dosing, cooling and inspection.
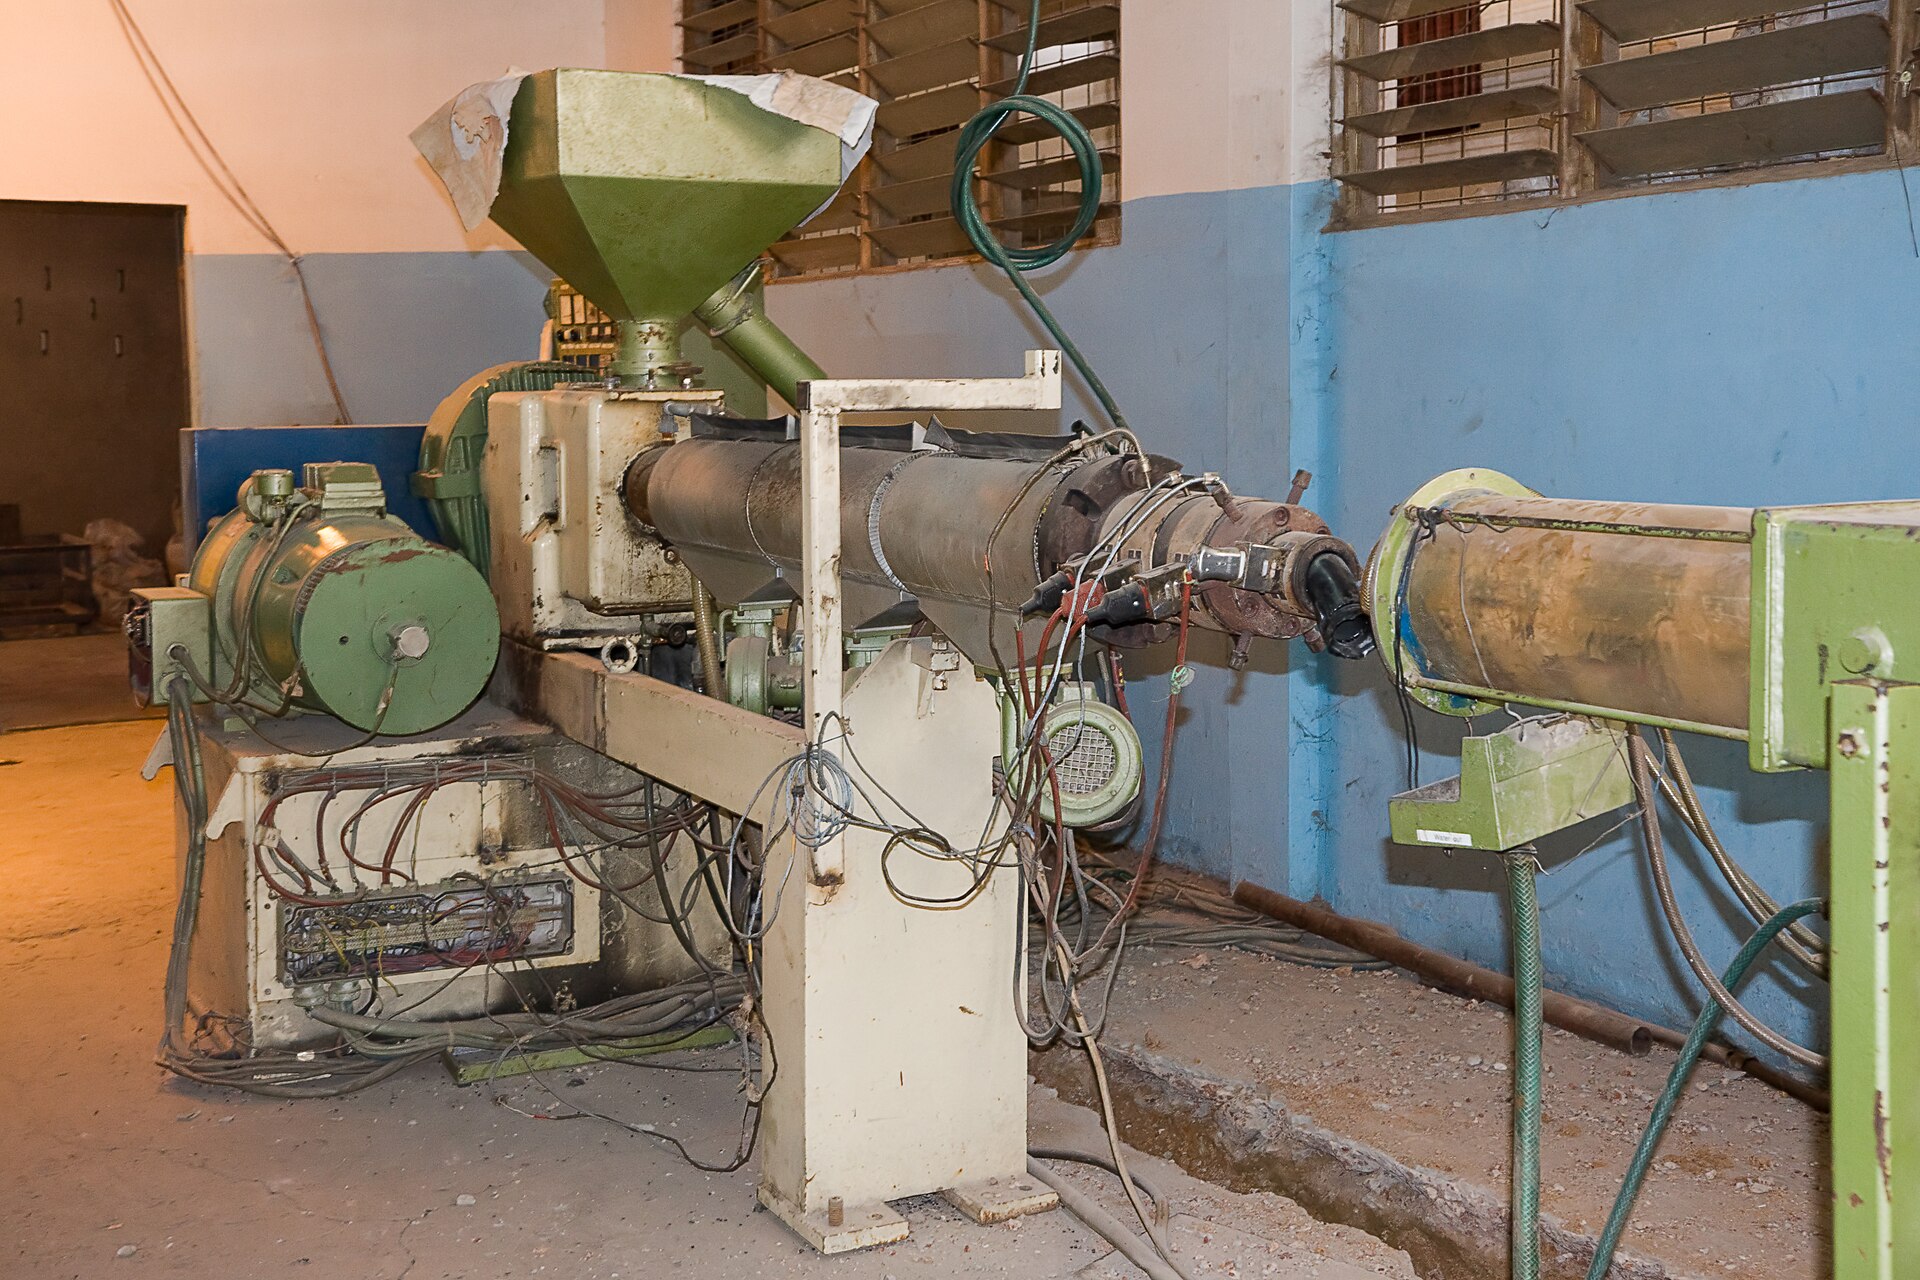
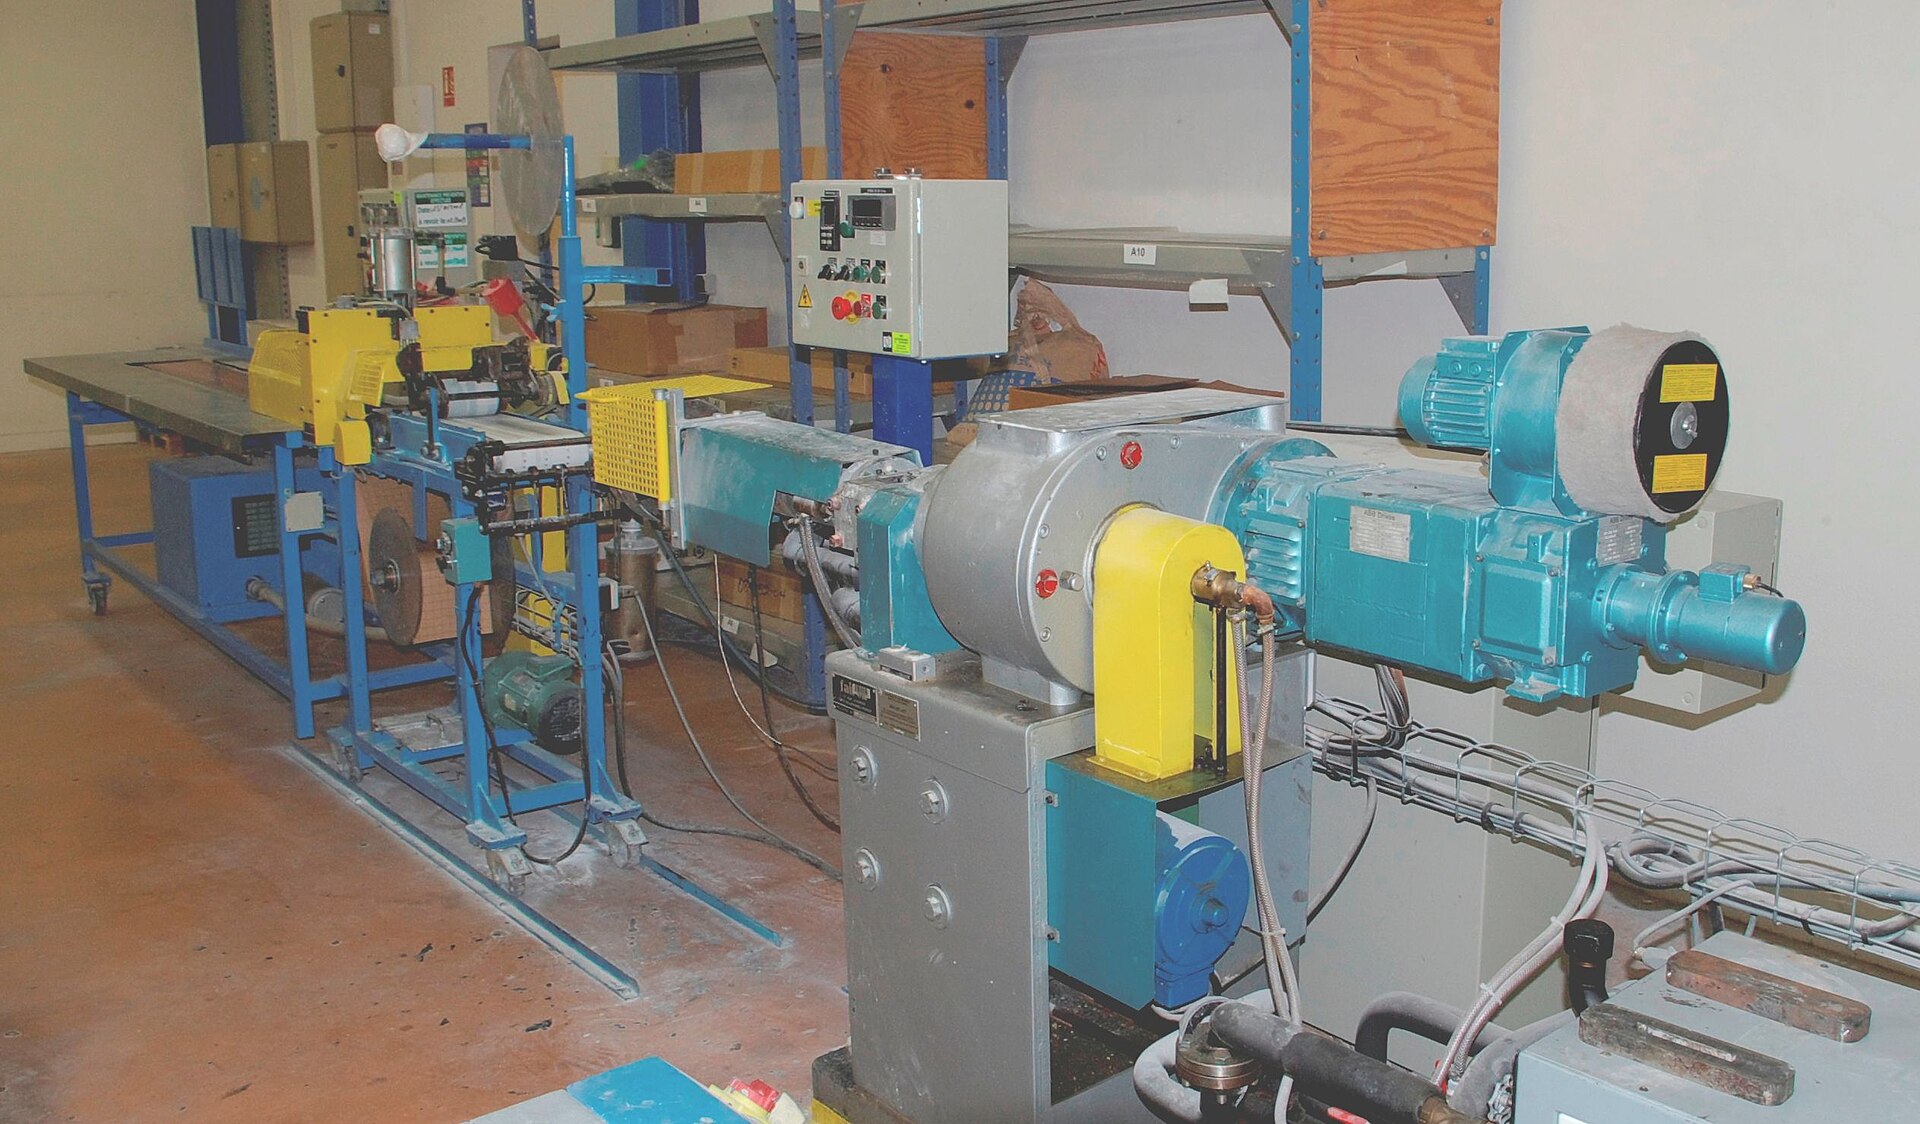
Pipe, profile, sheet, film or compounding lines with die, calibration, cooling, haul-off, cutting or winding.
HDPE/PP container extrusion blow moulding or PET preform reheating and stretch blow moulding.
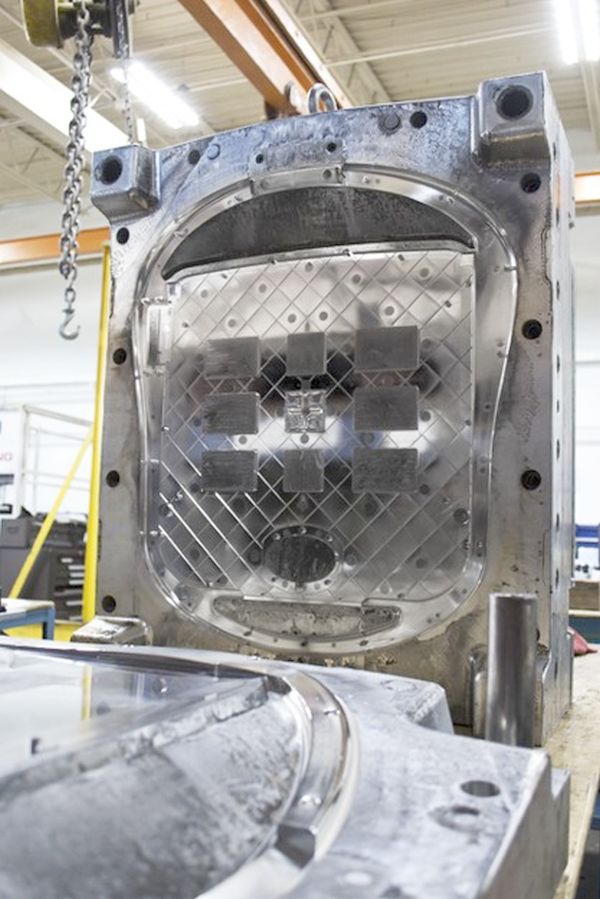
Product DFM, mould steel preparation, CNC, EDM, fitting, trial, maintenance and spare inserts.
Preliminary selection range only. Guaranteed output is calculated from resin, part weight, cycle, cavity count, dimensions, layer structure, OEE and utility conditions.
| Production route | Compact | Standard | High-output | Selection basis |
|---|---|---|---|---|
| Injection moulding | 50–250 t clamping | 250–1,000 t | 1,000–4,000+ t | Part mass, projected area, material, cycle and cavities |
| Pipe / profile / sheet extrusion | 50–250 kg/h | 250–800 kg/h | 800–2,500+ kg/h | Polymer, diameter/width, wall or gauge and die design |
| Blown / cast film extrusion | 50–200 kg/h | 200–600 kg/h | 600–1,500+ kg/h | Film width, gauge, layer count and resin recipe |
| Extrusion blow-moulded containers | 300–1,500 pcs/h | 1,500–6,000 pcs/h | 6,000–20,000+ pcs/h | Container volume, head count, material and trim |
| PET stretch blow moulding | 2,000–8,000 bottles/h | 8,000–30,000 bottles/h | 30,000–72,000+ bottles/h | Bottle size, cavities, preform and air system |
| Mould / tooling workshop | 2–8 mould sets/month | 8–20 mould sets/month | 20–50+ mould sets/month | Tool size, complexity, steel and trial-validation scope |
Yes. They are engineered as separate production cells sharing qualified utilities, material handling, laboratory and warehouse systems where practical.
Extrusion is normally selected by kg/h, while moulding output is validated in pieces/h from part mass, cavities, cycle and OEE.
Yes. Scope can include product DFM, new moulds/dies, trials, spare inserts, maintenance tools and an in-house tooling workshop.
Where product standards allow, the plant can include sorting, granulation, drying, filtration and controlled recycled-content dosing.
They can be: chilled water, cooling towers, low- and high-pressure air, power distribution, ventilation and material conveying.
After drawings, materials, cycle tests, utilities and acceptance criteria are confirmed in the technical agreement.
Send the product, material, target output, shifts and local utility data for a route-specific line balance.