1. Segregate and equalize
Identify free-oil, emulsion, chemical-cleaning and storm-water streams; contain spill and batch loads before downstream treatment.
 CHINA BENTEINDUSTRY GROUP
Oily and emulsified industrial wastewater treatment with separated free-oil recovery, emulsion breaking, DAF, polishing and sludge-management duties.
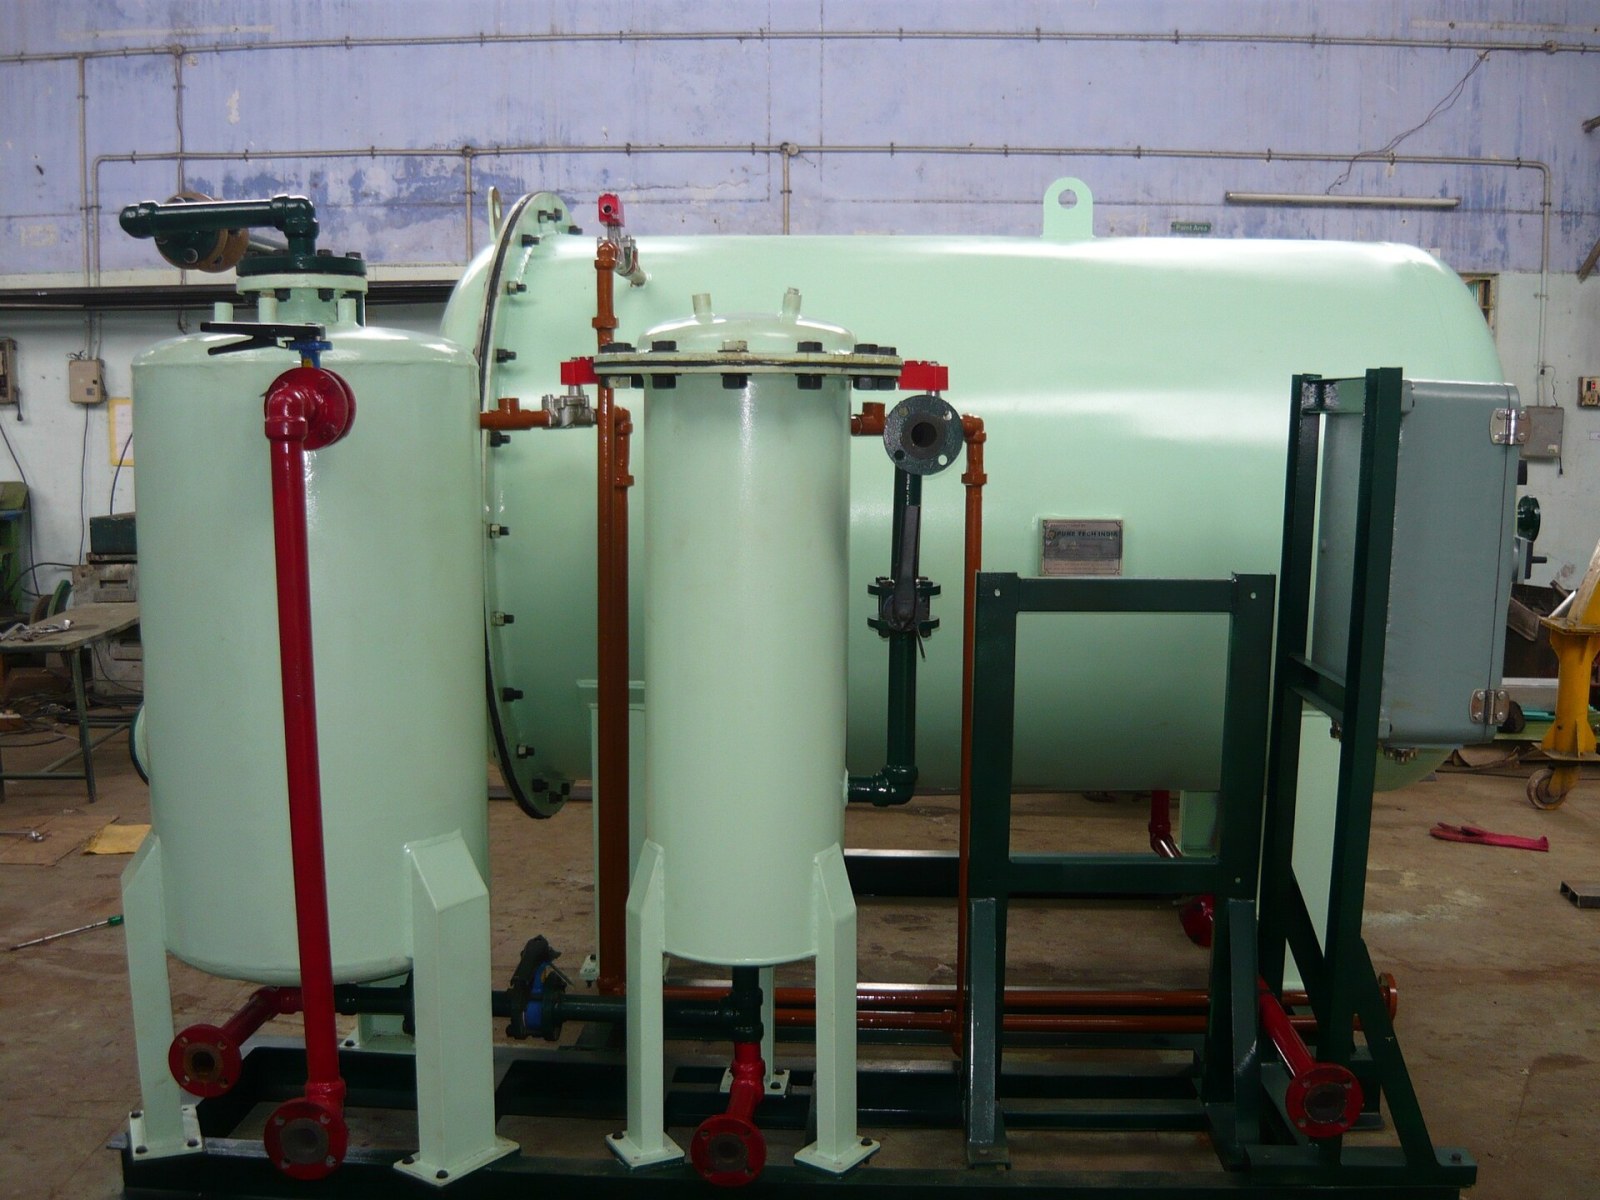
Engineering route for free oil, dispersed oil, stable emulsions, surfactants and fluctuating loads. Final configuration is based on representative sampling, treatability evidence and the agreed discharge or reuse target.
| Design question | Engineering response |
|---|---|
| Free oil | API/CPI separation, skimming or coalescing is selected from droplet size, flow and solids. |
| Stable emulsion | Jar testing defines pH adjustment, emulsion breaking, coagulation/flocculation and DAF duty. |
| Fine solids and float | DAF, clarification and sludge thickening are designed with polymer, solids and disposal data. |
| Residual COD | Biological, oxidation, carbon or membrane polishing follows oil removal where required by the final outlet. |
| Capacity basis | Average flow, peak wash-down flow, batch release and storm-water interfaces are confirmed separately. |
This category covers free oil, dispersed oil, stable emulsions, surfactants, fine solids and dissolved organics from process washing, equipment cleaning, metalworking, terminals and tank areas. Free oil, stable emulsion and dissolved COD require separate design decisions; they must not be treated as one contaminant.
Typical duties include refinery and terminal drains, machinery washing, maintenance wastewater, metalworking fluids, oily storm-water interfaces, tank-bottom water and process washwater. Segregation prevents clean storm water and high-strength emulsions from overloading the same treatment train.
Confirm average and peak flow, pH, temperature, oil and grease, free versus emulsified oil, surfactants, COD/TOC, suspended solids, salinity, metals, solvents, chemical additions and discharge target. Sampling must cover wash-down, batch discharge and rain-event conditions where they affect the oily sewer.
Selection begins with source segregation and treatability tests, then balances biological, physicochemical, membrane and thermal boundaries against residue outlets and acceptance requirements.
Identify free-oil, emulsion, chemical-cleaning and storm-water streams; contain spill and batch loads before downstream treatment.
Use gravity separation, coalescing or skimming where droplet size and solids loading support physical recovery.
Jar-tested chemical conditioning and DAF separate emulsified oil and fine solids; the selected chemistry is confirmed from actual wastewater.
Biological treatment, oxidation, adsorption or membranes are matched to residual COD, salinity, toxicity and water-reuse requirements.
Recovered oil, scum, dewatered sludge and spent media each receive a documented recovery, treatment or compliant-disposal route.


Main equipment: API/CPI separator, coalescer, chemical mixing, DAF, oil skimmer, biological and filtration packages.
Recovered oil, flotation scum, oily sludge, VOC and cleaning residues are handled separately.
Power, air, water, thermal utilities, chemical storage and consumption are calculated from the agreed flow and quality envelope. Off-gas, odor and ventilation controls are incorporated where the selected process requires them.
PLC/SCADA integrates critical instruments, alarms, interlocks, trends and operator controls. Capacity is defined by average, peak and batch flows, equalization strategy, production availability and redundancy requirements.
Major drivers include contaminant load and variability, materials of construction, footprint, redundancy, chemical and energy duties, sludge/concentrate outlet, automation level and the required discharge or reuse quality.
Customer inputs include verified analyses, process inventory, site layout, utility conditions, hazardous-area requirements, local codes and the acceptance sampling protocol. Outputs are agreed as treated water, recovered materials and managed residues at defined battery limits.
Related capabilities: Turnkey process plants, factory modernization, residue recovery, renewable energy and SMART monitoring.
A representative sampling program should cover flow, peaks, pH, temperature, COD/TOC, suspended solids, salts, priority pollutants, toxicity indicators and the intended discharge or reuse target.
The route is selected from wastewater characterization, treatability testing, flow variability, site constraints, residue outlets and the agreed acceptance basis.
Source segregation, emergency containment, equalization, controlled transfer and online monitoring are defined before downstream treatment.
Interfaces are selected from pretreatment, biological, physicochemical, membrane and thermal processes according to the wastewater-specific duty.
Sludge, flotation scum, spent media, concentrates and recovered materials are characterized, dewatered or contained, and routed to an approved recovery or disposal outlet.
Power, process water, air, steam or thermal energy, chemical storage, ventilation and drainage are calculated from the confirmed design basis rather than assumed values.
PLC/SCADA integration and online instruments are selected for critical parameters, alarms, interlocks, trend recording and controlled operation.
Performance criteria are agreed against the approved influent envelope, capacity, operating conditions, sampling method, analysis standard and discharge or reuse target.