
What it is
Controls modernization must preserve safe process behavior while moving obsolete hardware and software to a supportable architecture.
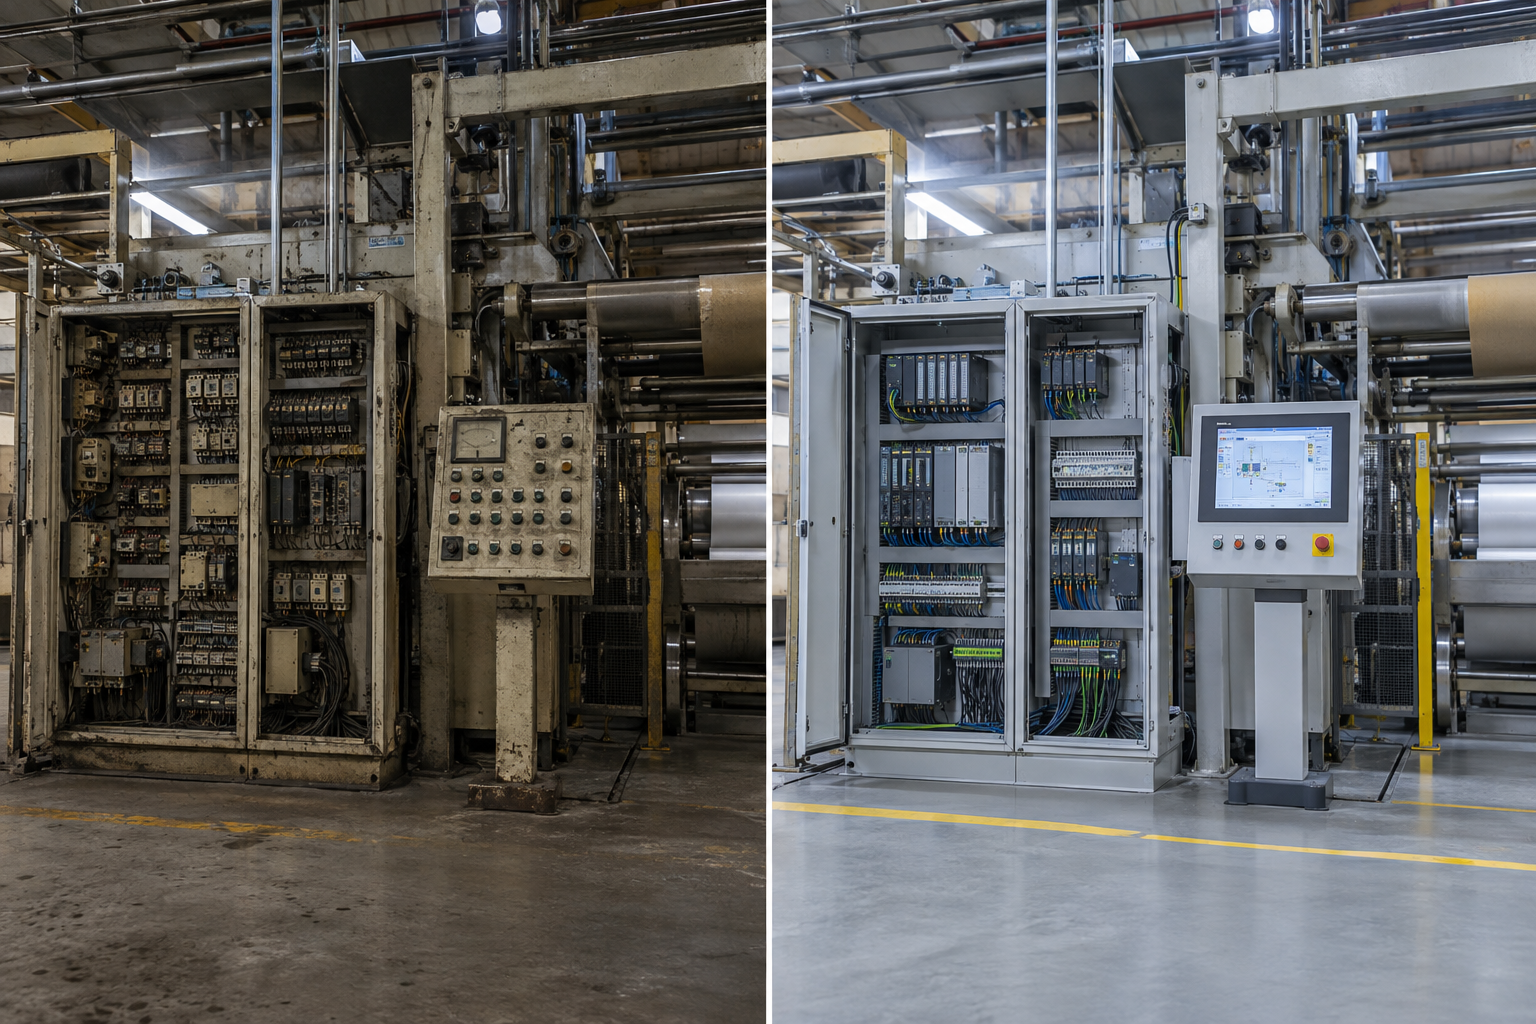
The project inventories field devices, panels, PLCs, HMI/SCADA, networks, alarms, historian and interfaces. It then defines a migration that maintains required interlocks, recipes, sequences and data while addressing obsolescence and access control.
Typical applications
- Obsolete PLC or HMI replacement
- SCADA consolidation and historian upgrade
- Network segmentation and secure remote support
- Migration with limited production shutdown
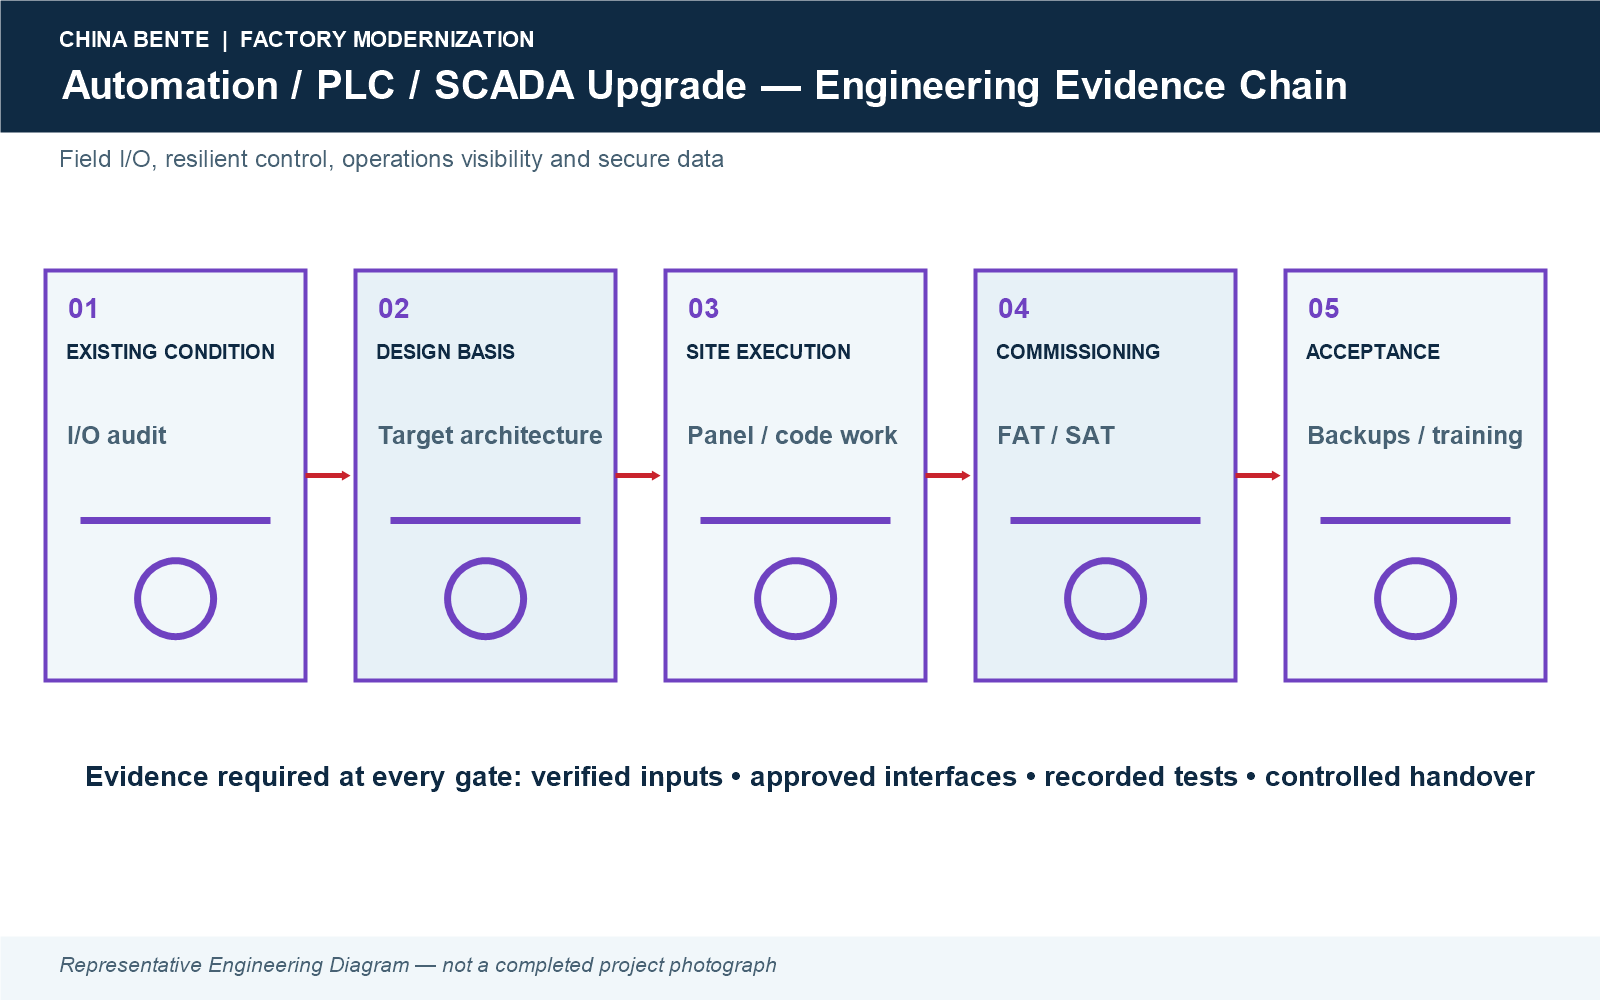
Representative engineering sequence. Final shutdown, cutover and performance criteria are agreed from verified plant data.
Main equipment and system architecture
- PLCs, remote I/O and control panels
- HMI/SCADA servers and operator stations
- Industrial switches, gateways and segmented networks
- Historian, alarms and approved reporting interfaces
- UPS, time synchronization and backup systems
- Secure engineering and remote-access interfaces
Capacity balance and design basis
Sizing uses verified I/O and tag count, scan and data rates, sequence criticality, alarm load, historian retention, users, availability and lifecycle support. Existing undocumented behavior remains an identified risk until tested.
Retained / replaced / interface matrix
| Category | Engineering basis |
|---|---|
| Retained | Suitable field devices, drives, instruments and infrastructure with verified signals, condition and support. |
| Replaced | Obsolete controllers, unsupported operator stations, unreliable panels or network components within the approved scope. |
| Interfaces | I/O marshalling, protocols, safety systems, drives, package units, databases, user roles, backups and enterprise handoffs. |
Utilities and site infrastructure
- Control power, UPS and grounding review
- Panel cooling and environmental conditions
- Fiber/copper network routes
- Server or virtualization resources where approved
- Secure backup and recovery storage
Customer engineering inputs
- Current source code and backups where available
- I/O lists, network drawings and panel records
- Cause/effect, sequences and alarm philosophy
- User, data and cybersecurity requirements
- Shutdown window and rollback requirements
Quality, automation and control
Configuration management, peer review, simulation, FAT/SAT, alarm rationalization, versioned backups and test records protect process behavior and traceability.
CAPEX and OPEX drivers
CAPEX is driven by I/O migration, panels, licenses, networks, engineering/testing and outage complexity. OPEX includes support, licenses, backups, cybersecurity maintenance and lifecycle replacement.
Safety, environmental and compliance
Safety-related functions are identified and governed separately; access control, change authorization, network segmentation, fail-safe states and rollback are incorporated.
Outputs and acceptance basis
Acceptance requires completed FAT/SAT, point-to-point and sequence tests, alarm/interlock checks, data validation, backups, documentation and training.
Shutdown, changeover and commissioning
Cutover is staged with frozen code, approved test packs, isolations, temporary operation where required and defined rollback points before restart.
Before / after evidence
No unverified availability or downtime reduction is claimed. Comparable approved references are listed through Projects & Cases.
Frequently asked questions
Can old PLC logic be copied directly?
Only after it is reviewed, verified and mapped to the target architecture and safety basis.
What if source code is missing?
The behavior must be reconstructed from field verification, documents and controlled testing, with risk explicitly managed.
Can migration be phased?
Yes, using defined interfaces and temporary coexistence where safe and supportable.
How is cybersecurity addressed?
Through segmentation, roles, secure access, backups, change control and the approved site policy.
What is included in FAT?
Hardware checks, logic, sequences, alarms, HMI, communications and simulated I/O as defined.
How are safety systems handled?
They remain subject to their applicable lifecycle and require independent verification where relevant.
Can SCADA integrate existing package units?
Yes when protocols, data ownership and control boundaries are verified.
What must be handed over?
Source files, backups, licenses, drawings, test records, settings and training materials.
Request a Project Evaluation
Share current drawings, operating records, constraints and the required future state. Any missing baseline or target remains TBC until verified.